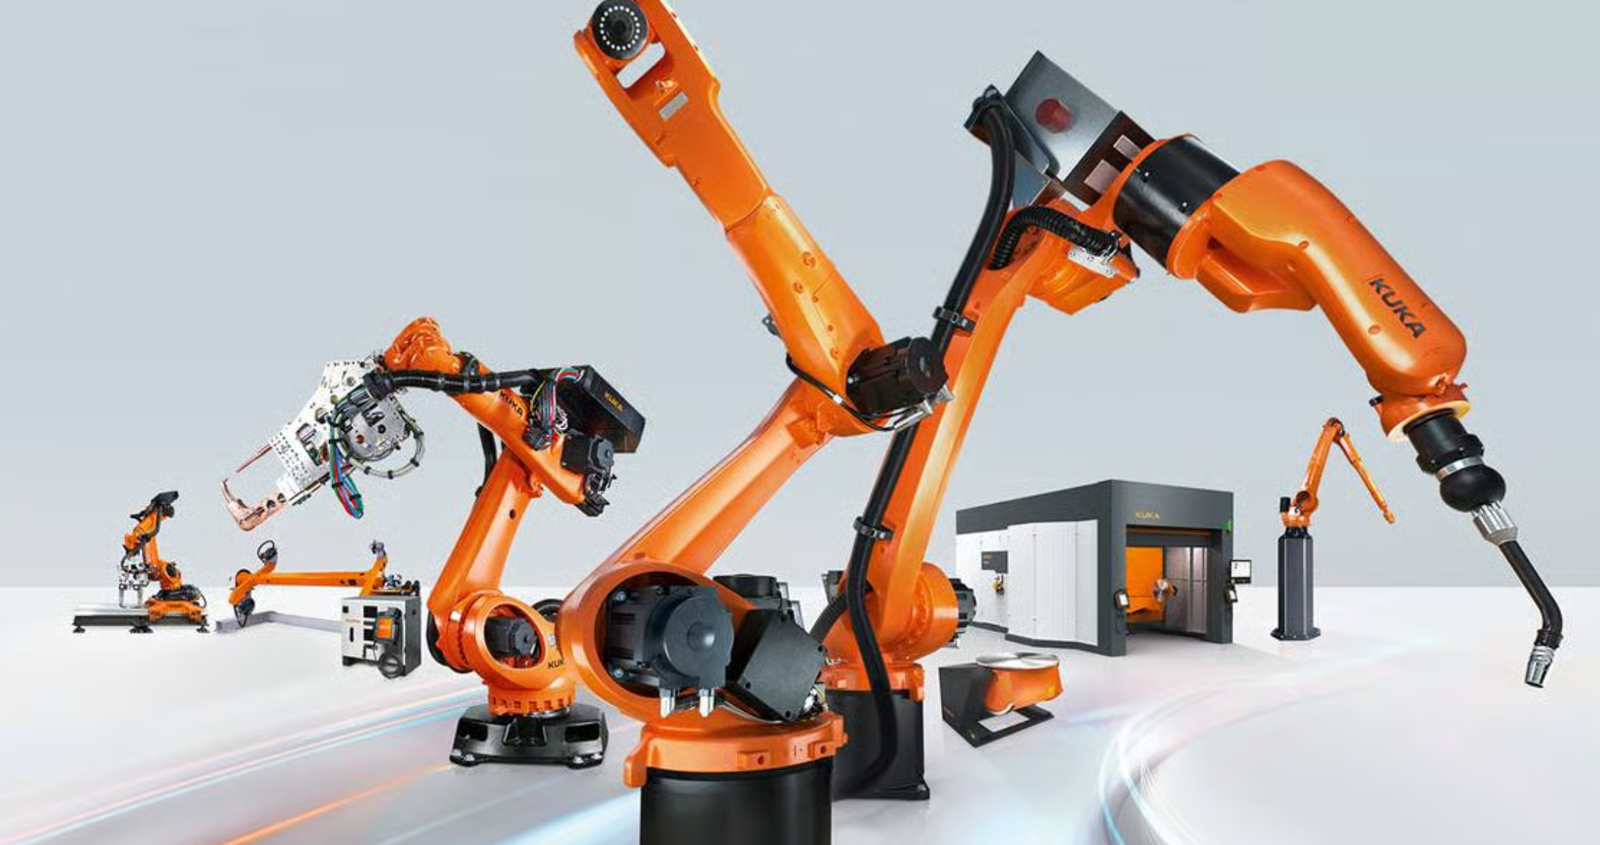
Quick answer:
- Why it pays: A robotic MIG/MAG cell keeps the arc on far longer than a manual welder — typically 70–85% arc-on time, against 20–30% for skilled manual welding.
- Cost: An entry single-robot MIG cell typically costs US$80,000–120,000. A dual-station cell with a 2-axis positioner and seam tracking costs US$150,000–220,000.
- Payback: For repeated steel frames with good fit-up, payback of 2–4 years is realistic. In the worked example below, it is about 3.7 years on labour savings alone.
| Manual MIG | Robotic MIG cell | |
|---|---|---|
| Arc-on time | 20–30% (about 25% typical) | 70–85% |
| Weld consistency | Depends on the welder | Repeatable when fit-up is controlled |
| Investment | Welding set + fixtures | US$80,000–220,000+ |
| Best for | One-offs, variable parts, repairs | Repeated parts and part families |
Source: The Fabricator — arc-on time for quoting welding jobs.
Thinking about automating frame welding? Send HORISTAR the frame size, material and thickness, monthly volume and a photo or drawing. We will check torch access, fixture and positioner needs, and quote a cell. Discuss Your Robotic Welding Project on WhatsApp
1. Is Your Steel Frame a Good Candidate?
| Condition | Verdict |
|---|---|
| Same frame repeated every week | Strong candidate |
| Families of similar frames | Good — with quick-change fixtures |
| Large frames with welds on several sides | Good — needs a positioner |
| Gaps vary by more than the process tolerance | Fix cutting and bending first, or add seam tracking |
| Every frame different | Weak — programming time eats the gain |
| Code welds (e.g. AWS D1.1) | Possible — qualify the robotic procedure first |
Rule: Robots repeat motion; they do not fix bad parts. Accurate laser cutting and bending upstream make robot welding work.
2. MIG, MAG and GMAW
- MIG (metal inert gas): argon or helium shielding — mainly aluminium.
- MAG (metal active gas): argon–CO₂ mixes or CO₂ — most carbon-steel frames.
- Both are GMAW.
Specify the base metal, wire and gas, not just “MIG”. Reference: TWI — What is MIG/MAG welding?
3. What a Robotic Welding Cell Costs
Published 2026 cost ranges for MIG cells:
| Cell type | Typical price |
|---|---|
| Entry: one robot, simple positioner, power source, fencing | US$80,000–120,000 |
| Cobot welding cell | US$60,000–120,000 |
| Dual-station cell with 2-axis positioner and seam tracking | US$150,000–220,000 |
| High-production / multi-station | US$280,000–450,000+ |
Typical component breakdown for a dual-station MIG cell:
| Component | Range |
|---|---|
| Industrial robot arm | US$40,000–80,000 |
| Dual-station positioner | US$20,000–45,000 |
| Safety enclosure | US$15,000–30,000 |
| Fixturing | US$10,000–40,000 |
| Integration and programming | US$20,000–40,000 |
Budget 10–20% of cell cost for fixtures. Running costs (consumables, maintenance) are typically US$5,000–15,000 a year.
These are published industry ranges, not HORISTAR quotations — see the HORISTAR Robotic Welding Machine Cost Guide.
4. Fixtures Come Before the Robot
A fixture must:
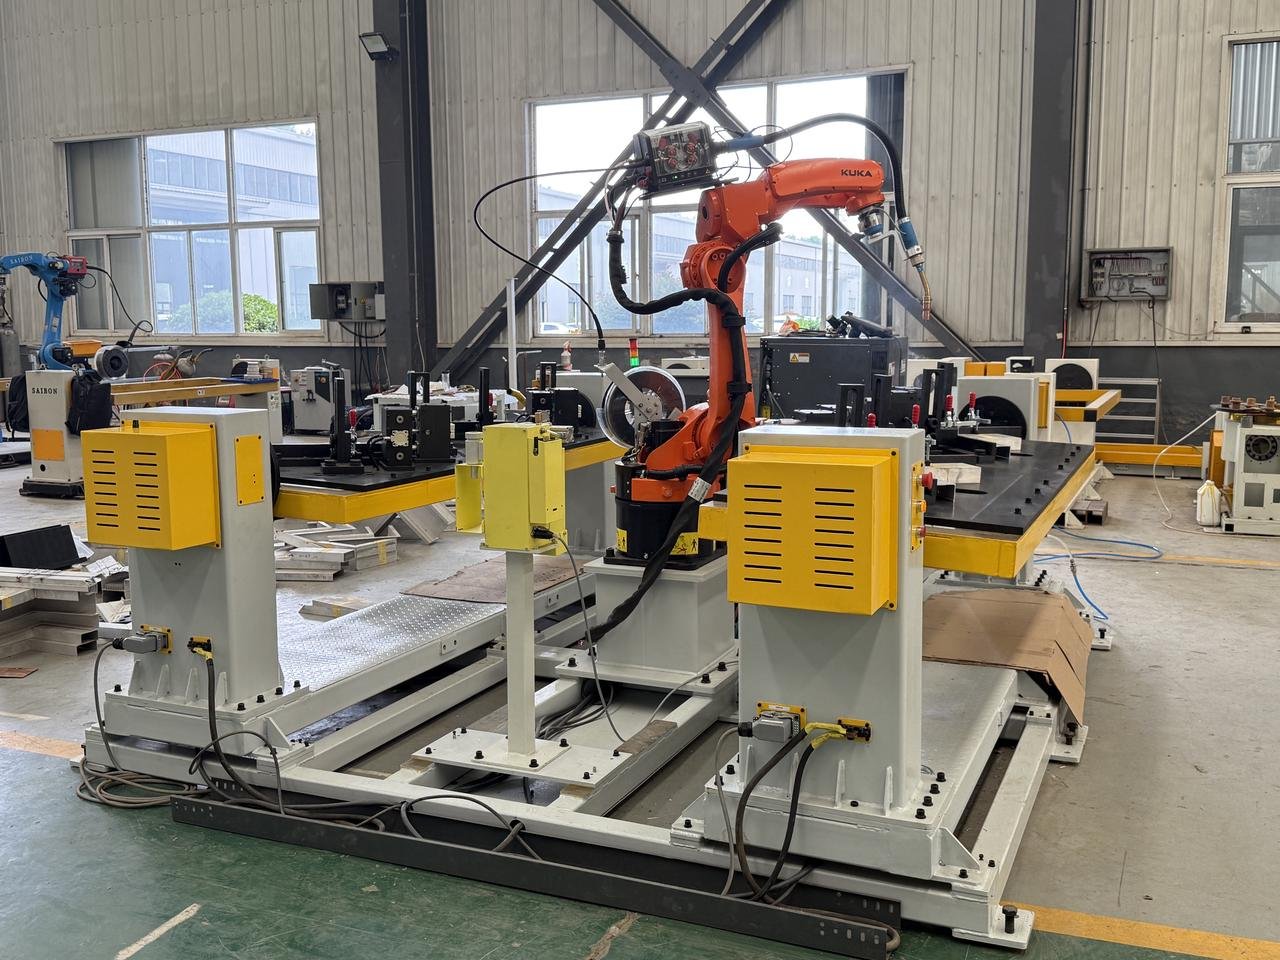
- Locate each part from a repeatable datum
- Hold parts without blocking the torch
- Allow for heat distortion
- Load and unload quickly and safely
Torch access check: nozzle and torch body clearance, wire approach angle, weld start and stop points, and robot wrist orientation. A fixture that blocks one weld forces manual rework on every part.
5. Do You Need a Positioner?
| Set-up | When |
|---|---|
| Fixed table | All welds reachable from one side |
| Single-axis positioner (rotation) | Welds on several sides of a long frame |
| Two-axis positioner (tilt + rotate) | Complex 3D frames |
| Dual-station (two fixtures) | Operator loads one side while the robot welds the other — raises arc-on time |
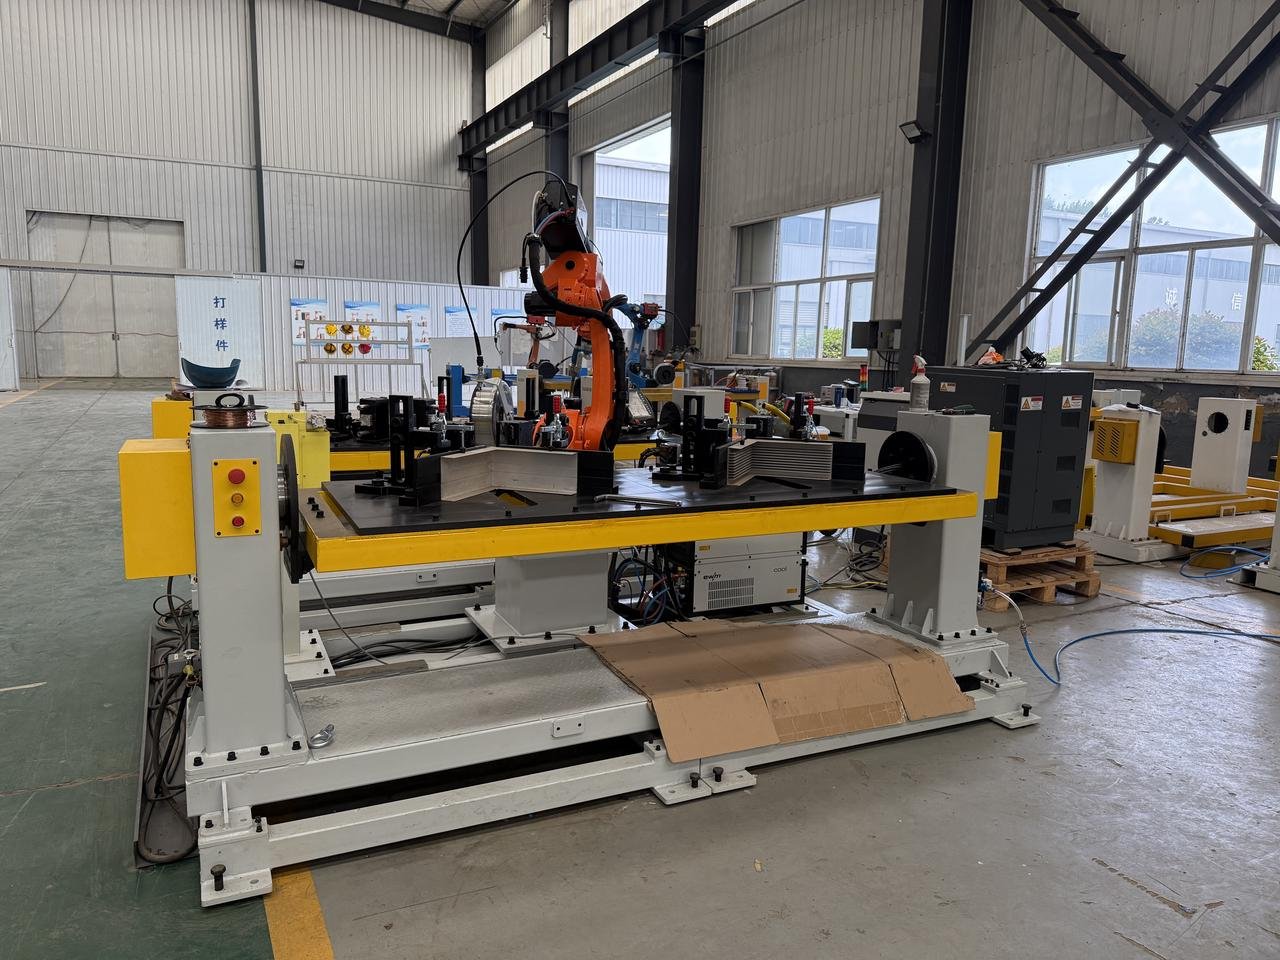
Load rating is more than weight. Check combined part + fixture weight, centre of gravity, overturning moment and inertia.
6. HORISTAR RW-10: What the Numbers Mean
| Published RW-10 parameter | Value | What it means |
|---|---|---|
| Robot wrist payload | 10 kg | Torch, cable and sensors — not the workpiece |
| Maximum reach | 2,018 mm | Reach envelope; torch angle may limit usable reach |
| Positioner load capacity | 1,000 kg | Part + fixture, subject to centre of gravity |
| Positioner rotation diameter | 1,000 mm | Largest swing diameter |
| Positioner rotation | ±180° | Lets the robot reach several sides |
Source: HORISTAR Robot Welding Machine.
Ask for a reach study with your actual frame before ordering.
7. Seam Finding and Tracking
| Method | What it corrects | Limits |
|---|---|---|
| Touch sensing | Part position offsets before welding | Adds seconds per weld |
| Through-arc tracking | Joint drift during weaving welds | Needs suitable joint and weave |
| Laser seam sensor | Joint position and gap | Higher cost; sensitive to spatter and surface |
Sensing helps with small variation; it does not replace accurate parts. More: HORISTAR seam finding and tracking guide.
8. Cycle Time and Output: Worked Example
Repeated steel frame. Manual welding takes 20 minutes per accepted frame.
Robotic single-station cycle:
| Step | Time |
|---|---|
| Load and clamp | 2.5 min |
| Arc-on welding | 5.5 min |
| Robot moves | 1.5 min |
| Unload | 1.0 min |
| Inspection and cleaning | 2.0 min |
| Total | 12.5 min |
Shift output with 420 planned minutes at 85% availability (357 minutes):
| Manual | Robot, single station | |
|---|---|---|
| Frames per shift | 357 ÷ 20 = 17.9 | 357 ÷ 12.5 = 28.6 |
| Gain | — | +60% |
Arc-on time here is 5.5 ÷ 12.5 = 44%. A dual-station cell overlaps loading with welding and pushes arc-on time toward the 70–85% range, cutting the effective cycle further.
Want this calculation for your frame? Send HORISTAR your current manual time per frame and monthly volume. We will estimate robot cycle time and output. Estimate My Robot Cycle Time
9. ROI: A Reproducible Example
| Input | Value |
|---|---|
| Annual frames | 5,000 |
| Manual labour per frame | 20 min |
| Robot cell labour per frame (loading, checks) | 8 min |
| Labour saved per frame | 12 min |
| Loaded labour cost | US$28/h |
| Incremental investment | US$85,000 (entry-cell range) |
| Extra operating cost | US$5,000/year |
- Labour hours saved: 5,000 × 12 ÷ 60 = 1,000 h/year
- Labour value: 1,000 × US$28 = US$28,000
- Net of operating cost: 28,000 − 5,000 = US$23,000/year
- Simple payback: 85,000 ÷ 23,000 ≈ 3.7 years
Payback improves with two shifts, higher labour costs, or extra sales from the added capacity. It only becomes real cash if the freed hours are actually redeployed or saved.
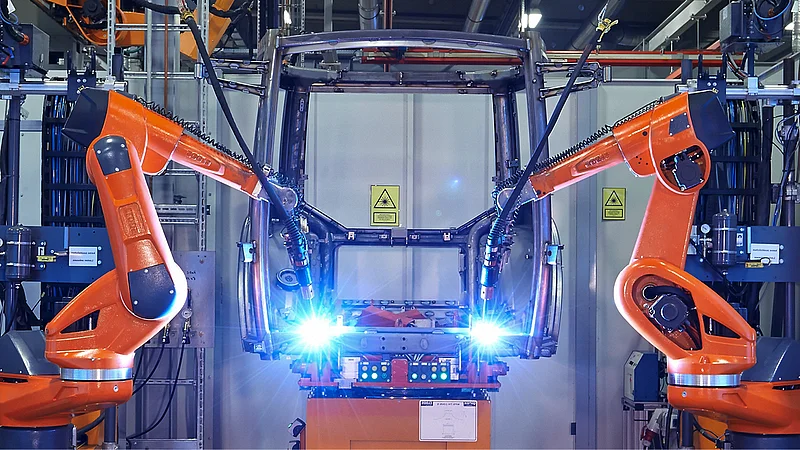
10. Weld Quality and Codes
- Qualify the welding procedure: base metal, wire, gas, current, voltage, travel speed and position.
- For structural steel under contract, AWS D1.1/D1.1M:2025-AMD1 may apply.
- Accept parts on visual inspection, weld size, dimensions and any required NDT.
- Run a repeatability trial on several frames — one good weld proves little.
Reference: AWS D1.1.
11. Safety
Robot welding cells combine robot motion hazards with arc radiation, fumes and hot metal.
Relevant standards: ISO 10218-2:2025 (robot cells), AWS D16.1M/D16.1:2026 (robotic arc welding safety), AWS D16.3:2026 (risk assessment) and OSHA 29 CFR 1910.252 in the US.
Sources: ISO 10218-2:2025; AWS D16 committee; OSHA 1910.252.
12. What a Complete Quote Should Include
| Area | Check |
|---|---|
| Robot | Brand, model, reach, payload |
| Welding package | Power source, wire feeder, torch, cleaning station |
| Fixtures | Design, quantity, change parts |
| Positioner | Axes, load, coordinated motion or indexing |
| Sensing | Touch / arc / laser tracking |
| Safety | Fencing, interlocks, light curtains, fume extraction |
| FAT | Sample parts and acceptance criteria |
| Installation and training | Who does what on site |
Frequently Asked Questions
How much does a robotic MIG welding cell cost?
Entry single-robot cells typically cost US$80,000–120,000. Dual-station cells with positioners and seam tracking cost US$150,000–220,000, and multi-station systems more.
What arc-on time does a welding robot achieve?
Typically 70–85% in a well-run cell, compared with 20–30% for skilled manual welders.
Is robotic MIG welding suitable for structural steel?
Yes, when the joint, procedure and fit-up are suitable and the procedure is qualified to the governing code.
Do I need a positioner?
Only if the robot cannot reach every weld with the part in one position. Large frames welded on several sides usually need one.
What payback can I expect?
About 2–4 years for repeated parts with controlled fit-up. The example above gives 3.7 years on labour savings alone.
Can one cell weld several products?
Yes, with separate programs and fixtures. Include fixture and programming cost per product in the ROI.
Discuss Your Steel Welding Project with HORISTAR
Send workpiece dimensions + material and thickness + monthly volume + destination country, plus a photo or drawing.
Discuss Your Robotic Welding Project on WhatsApp
Explore the HORISTAR Robot Welding Machine.
Technical Sources
- The Fabricator — arc-on time for quoting welding jobs
- TWI — MIG/MAG · AWS D1.1 · ISO 10218-2:2025 · OSHA 1910.252
- HORISTAR RW-10 product information
Cell cost ranges are published industry figures, not HORISTAR prices. Cycle-time and ROI examples use stated assumptions.