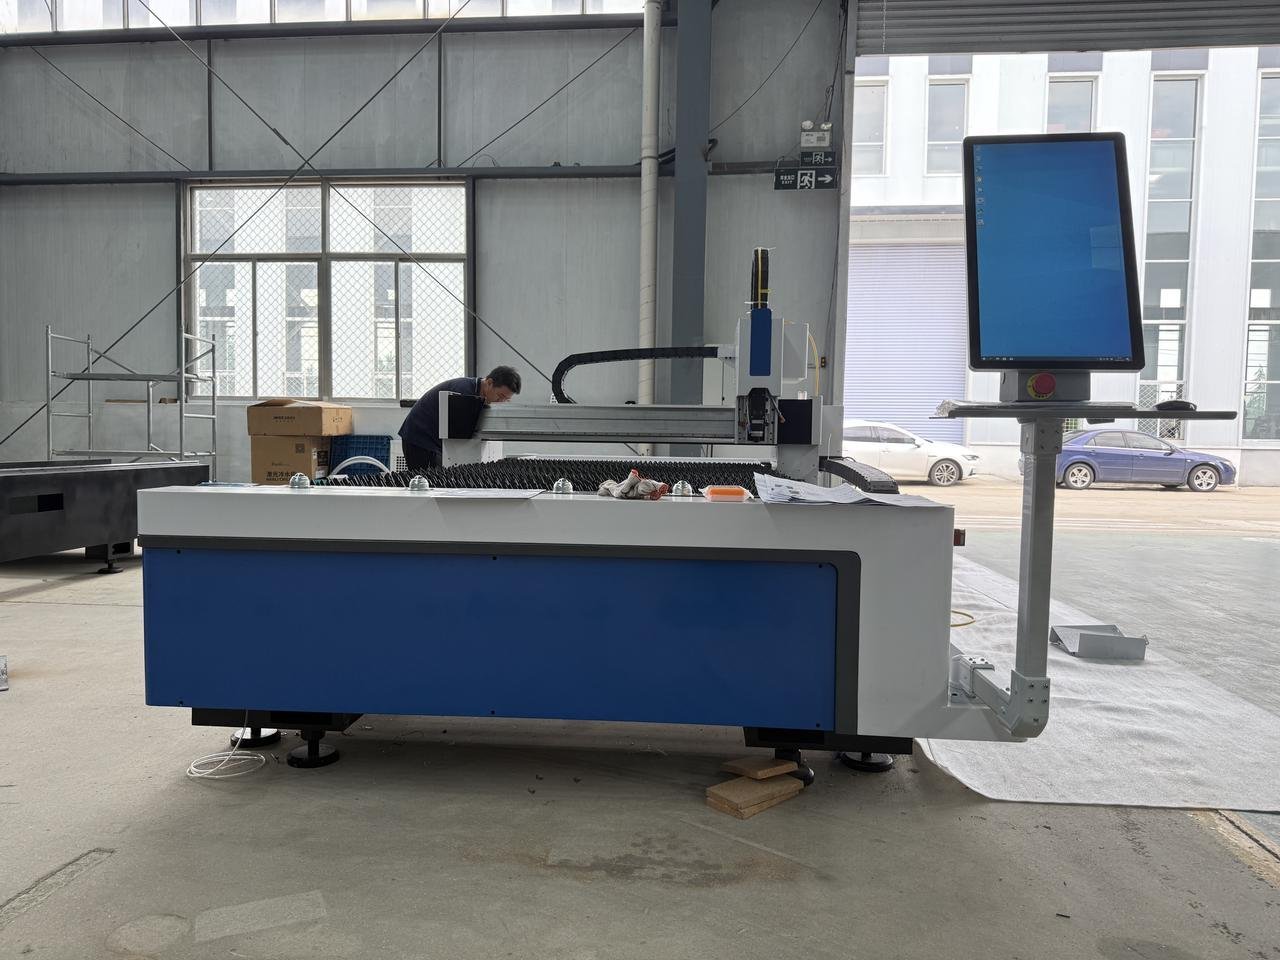
Quick answer:
- Thickness and speed: With nitrogen, a 3 kW fiber laser cuts stainless steel up to about 10 mm, a 6 kW up to about 20 mm. At 3 mm, typical speeds are 7–10 m/min (3 kW) and 15–18 m/min (6 kW).
- 304 vs 316: 316 contains 2–3% molybdenum for better chloride resistance. It cuts with the same machine and gas, so choose the grade for the product’s environment.
- Gas: Use nitrogen (about 10–20 bar) for bright, oxide-free edges, or compressed air where slight discoloration is acceptable.
| Stainless thickness | 3 kW speed (N₂) | 6 kW speed (N₂) | Recommended power |
|---|---|---|---|
| 1 mm | 28–35 m/min | 40–50 m/min | 1.5–3 kW |
| 2 mm | 18–24 m/min | 25–30 m/min | 3 kW |
| 3 mm | 7–10 m/min | 15–18 m/min | 3 kW (6 kW about 2× faster) |
| 6 mm | 2.0–2.7 m/min | 6–7 m/min | 6 kW (about 3× faster) |
| 8 mm | 1.0–1.2 m/min | 3.5–3.8 m/min | 6 kW |
| 10 mm | 0.5–0.6 m/min | 1.6–2.0 m/min | 6 kW |
| 12–20 mm | — | 1.2 to 0.2 m/min | 6 kW or higher |
Cutting 304 or 316 stainless? Send HORISTAR your grade, thickness range, sheet size and destination country. We will recommend the power, gas set-up and machine. Discuss Your Stainless Cutting on WhatsApp
1. 304 vs 316 Stainless Steel: What Changes?
| 304 | 316 | |
|---|---|---|
| Chromium | 17.5–19.5% | 16–18% |
| Nickel | 8–10.5% | 10–14% |
| Molybdenum | — | 2–3% |
| Main advantage | General corrosion resistance, lower price | Better resistance to pitting in chloride (sea air, salt, some chemicals) |
| Typical uses | Enclosures, kitchen equipment, panels | Marine, chemical, pharmaceutical, coastal architecture |
| Laser cutting | Same process | Same process |
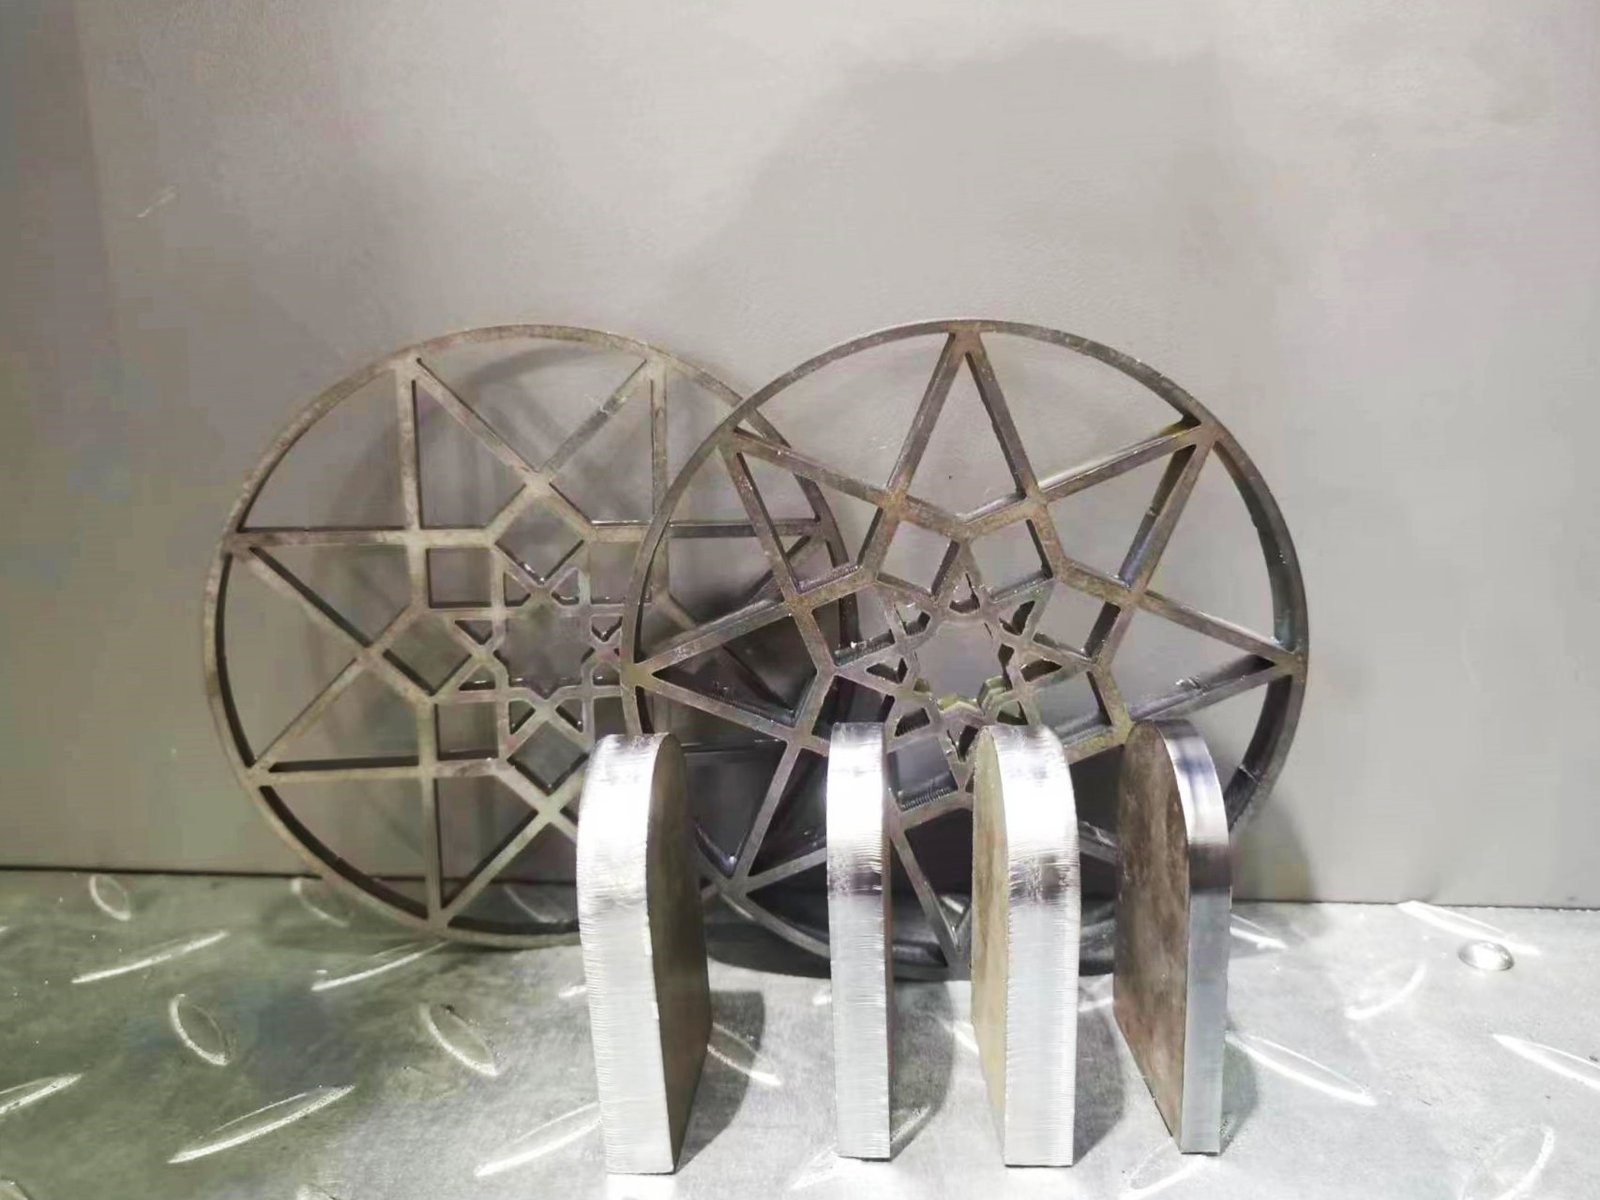
Composition per ASTM A240. The Nickel Institute notes molybdenum as the main reason for 316’s better localized corrosion resistance.
Does 316 need more laser power? No fixed rule. Cutting speed depends more on thickness, surface and gas than on the grade. If you cut both grades, test both at your thickness.
304L and 316L (low carbon) are used where parts will be welded. They cut the same way.
2. Nitrogen vs Compressed Air
| Nitrogen | Compressed air | |
|---|---|---|
| Edge colour | Bright, oxide-free | Slightly darker or yellowish |
| Typical pressure | 10–12 bar thin sheet; 16–20 bar thick | Compressor-dependent |
| Gas flow | about 18 m³/h (1.5 mm nozzle) to about 75 m³/h (3.0 mm nozzle) | Similar volumes, from your compressor |
| Cost driver | Purchased or generated nitrogen | Compressor electricity, dryer, filters |
| Best for | Visible parts, food equipment, parts to be welded | Hidden parts, parts that will be painted |
Air contains about 21% oxygen, so it oxidizes the cut edge slightly. It works if the edge meets your product specification. Air must be clean, dry and oil-free.
3. How Much Laser Power for Stainless?
Choose from your regular thickness, not the occasional maximum:
| Your regular stainless work | Power |
|---|---|
| Mostly 0.5–3 mm sheet | 1.5–3 kW |
| Regular 3–6 mm | 6 kW (2–3× faster than 3 kW) |
| Regular 6–12 mm | 6 kW+ |
| Regular 12–20 mm | 6 kW at the limit; 12 kW+ for production |
Maximum vs production thickness: A 3 kW machine’s stable stainless production range is about 6–8 mm, though it can reach 10 mm. A 6 kW machine runs about 10–15 mm reliably.
See also the HORISTAR Fiber Laser Power and Thickness Selection Guide.
4. Five Edge Problems and What Causes Them
| Problem | Common causes | Check |
|---|---|---|
| Bottom burr / dross | Gas pressure too low, speed too high, focus too high, worn nozzle | Burr height along the part |
| Rough edge | Unstable speed, wrong focus | Striation pattern |
| Discoloration | Oxygen in gas (air or impure N₂), heat build-up | Edge colour vs spec |
| Distorted small holes | Piercing too hot, holes smaller than thickness | Roundness and taper |
| Results vary across the sheet | Sheet not flat, height control | Cut test at several positions |
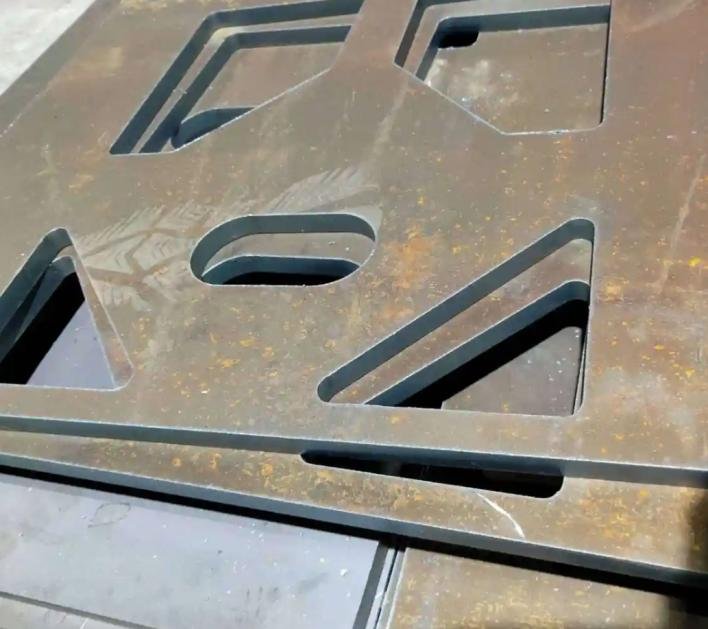
For specifying cut quality, ISO 9013:2017 (+ Amd 1:2024) covers laser cuts from 0.5 to 32 mm. Name the tolerance class on the drawing rather than writing “ISO quality”.
Sources: ISO 9013:2017, Amendment 1:2024.
5. Cost per Accepted Part: Nitrogen vs Air
Cost per accepted part = total production cost ÷ accepted parts
Worked example (24 parts per sheet, 18 minutes of gas-on time):
| Input | Value |
|---|---|
| Nitrogen flow | 28 Nm³/h (within the 18–75 m³/h range above) |
| Nitrogen price (assumed) | US$0.18/Nm³ |
| Extra compressor load for air | 12 kW |
| Electricity price (assumed) | US$0.15/kWh |
| Nitrogen | Air | |
|---|---|---|
| Gas or power cost per sheet | 28 × 0.18 × 0.30 h = US$1.51 | 12 × 0.15 × 0.30 h = US$0.54 |
| Per part | US$0.063 | US$0.023 |
| Extra edge finishing per part | none | US$0.10 (assumed) |
| Total per part | US$0.063 | US$0.123 |
Air looks cheaper until finishing is added. If your edges need no finishing, air wins. If they do, nitrogen wins.
Replace the assumptions with your local nitrogen and electricity prices.
Want to compare nitrogen and air on your own part? Send HORISTAR a DXF and your gas prices. We will estimate cost per part both ways. Compare Gas Cost per Part
6. Match the Edge to the Product
| Product | What matters | Gas |
|---|---|---|
| Electrical enclosures | Hole accuracy, burr-free | N₂ or air |
| Food processing equipment | Clean, oxide-free edges; later passivation | N₂ |
| Architectural panels | Edge appearance, surface protection | N₂ |
| Machinery parts | Fit and weld prep | Air often fine |
| Marine or chemical (316) | Corrosion after fabrication | N₂, then passivate |
A bright laser edge does not make a part food-safe or corrosion-proof. Follow the product’s cleaning and passivation requirements.
7. HORISTAR Machines for Stainless Steel
| Range | Models | Type |
|---|---|---|
| HM-S single-table | HM-S3015, HM-S4020, HM-S6025 | Open single table — flexible, lower cost |
| HM-FC enclosed | HM3015FC, HM2060FC | Enclosed cabin — safety, fume control, high-power options |
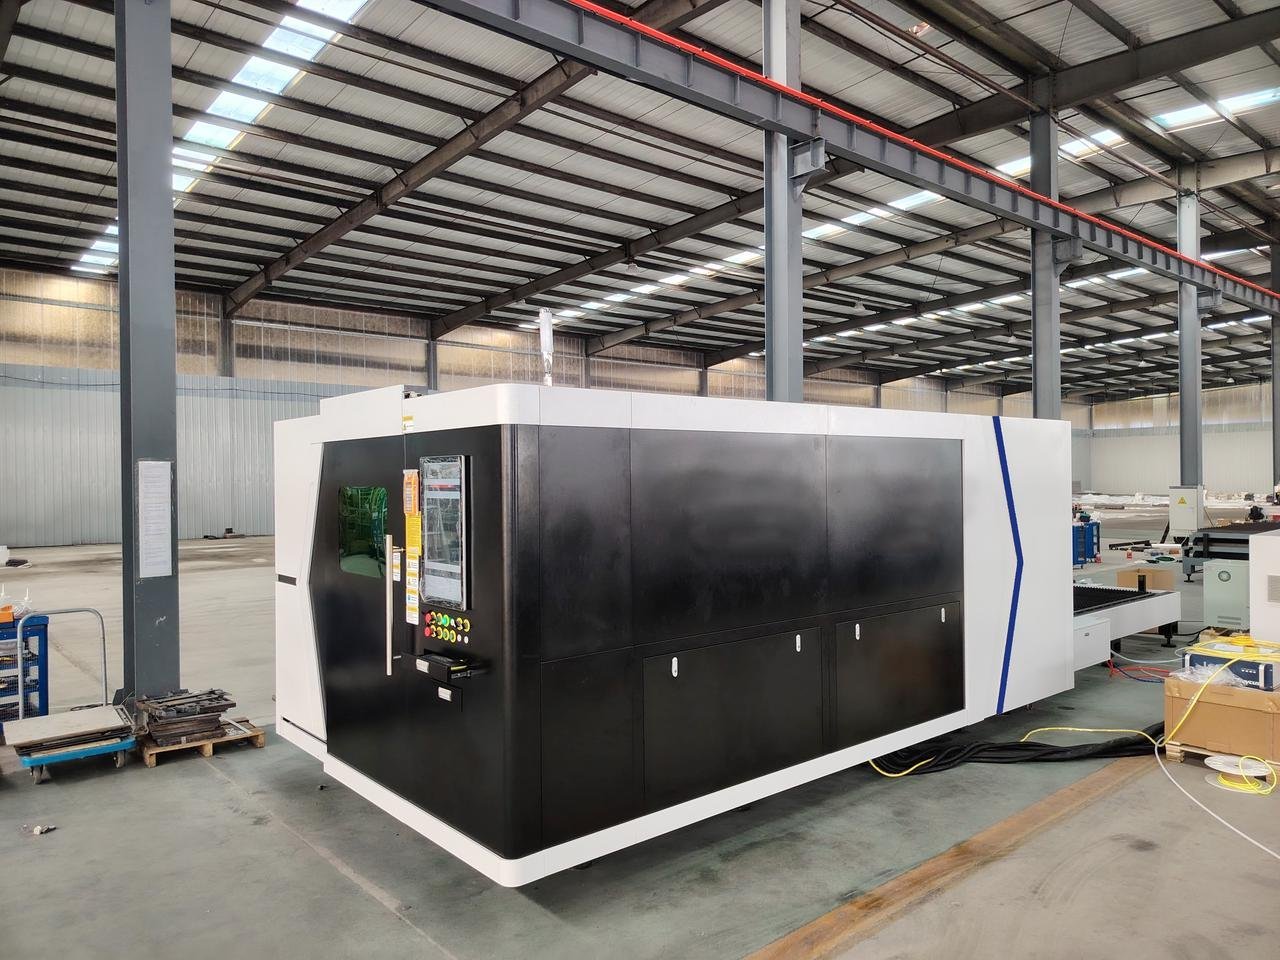
Explore Single-Table Fiber Laser Cutters and Enclosed Fiber Laser Cutters.
What a HORISTAR quotation lists: model and working area, laser source brand and power, cutting head, controller and nesting software, gas requirements, safety equipment, utilities and acceptance criteria.
8. Sample Cutting Test: How to Do It
- Send your actual 304/316 sheet, grade and finish.
- Include a part with small holes, slots and sharp corners — not a plain square.
- Cut with nitrogen and, if relevant, air.
- Measure burr, edge colour, hole size and accepted parts per sheet.
- Record cut time per sheet and gas use.
Frequently Asked Questions
How thick can a fiber laser cut stainless steel?
About 10 mm at 3 kW and 20 mm at 6 kW with nitrogen. Stable production thickness is lower: about 6–8 mm at 3 kW and 10–15 mm at 6 kW.
How fast does a fiber laser cut 3 mm stainless steel?
About 7–10 m/min at 3 kW and 15–18 m/min at 6 kW with nitrogen.
Does 316 stainless need more laser power than 304?
Not as a rule. Both are austenitic stainless steels and cut with the same process. Test both if you use both.
Is nitrogen required for stainless steel cutting?
Only when you need oxide-free edges. Compressed air works where slight discoloration is acceptable.
What nitrogen pressure is used for stainless steel?
About 10–12 bar for thin sheet and 16–20 bar for thick sections, depending on machine and nozzle.
How much nitrogen does laser cutting use?
Roughly 18 m³/h with a 1.5 mm nozzle up to about 75 m³/h with a 3.0 mm nozzle.
What should I send for a quotation?
Grade, thickness range, sheet size and destination country. A DXF and monthly volume help us recommend the configuration.
Discuss Your Stainless Steel Cutting with HORISTAR
Send material grade + thickness range + sheet size + destination country. Add a drawing and the required edge finish if available.
Discuss Your Stainless Steel Cutting Project on WhatsApp
Explore the HORISTAR Laser Cutting Machine Range.
Technical Sources
Speeds are another manufacturer’s published starting parameters, not HORISTAR test results. Gas and electricity prices in the cost example are assumptions.